Environmental & Climate Chamber Manufacturers – Top Indian Supplier
Choosing the right environmental chamber manufacturer affects testing accuracy, reliability and long-term equipment performance.
Indian industries increasingly require controlled environmental testing. Automotive, aerospace, defence, electronics, EV, pharmaceutical and industrial manufacturers all depend on reliable testing systems.
Several environmental chamber manufacturers operate in India. However, their product portfolios, engineering capabilities, customisation options and testing infrastructure differ.
What Makes A Good Environmental Chamber Manufacturer?
A capable manufacturer should understand more than chamber fabrication.
The manufacturer should understand the actual testing application. This includes temperature requirements, humidity conditions, chamber volume, product heat load, test cycles and applicable standards.
Engineering capability is equally important. A manufacturer should be able to design suitable heating, refrigeration, humidity, airflow and control systems.
Customisation is another important factor. Industrial applications often require non-standard dimensions, special temperature ranges, higher heat loads or integrated automation.
After-sales support also matters. Installation, commissioning, calibration, maintenance and technical support directly affect chamber uptime.
Therefore, manufacturers should be evaluated on engineering capability rather than price alone.
Top Indian Environmental Chamber Manufacturer
India has several established manufacturers serving environmental testing requirements. The following companies represent different strengths within the Indian market.
Comet Environs is an Indian manufacturer specialising in environmental testing systems.
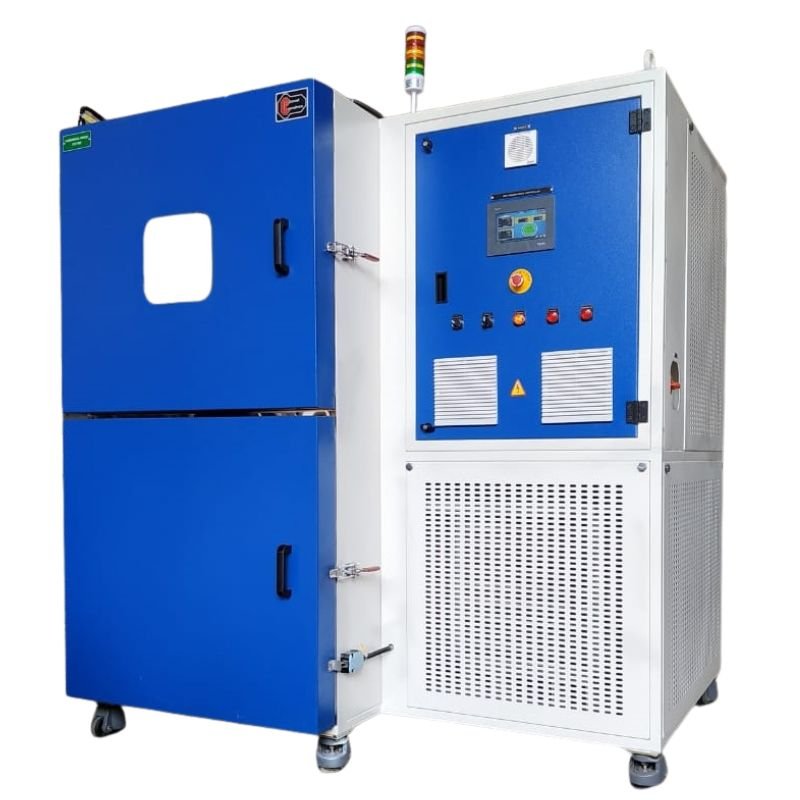
The company was founded in Bengaluru in 1987. It has more than four decades of experience in environmental testing solutions. Its portfolio includes environmental test chambers, climate test chambers, temperature and humidity chambers, thermal shock chambers, rapid cycling chambers, battery test chambers, sub-zero chambers and walk-in systems.
A major Comet advantage is its combination of chamber manufacturing and environmental testing infrastructure.
Its Bengaluru facility includes a 14,000+ sq. ft. testing and manufacturing environment. The company also operates an ISO/IEC 17025:2017 NABL-accredited testing laboratory and states DGAQA certification.
Comet also develops customised environmental chambers. These solutions can be designed around product dimensions, temperature requirements, humidity conditions, testing standards and application-specific requirements.
Its systems support industries including automotive, EV, aerospace, defence, electronics, semiconductors, pharmaceuticals and medical devices.
Best suited for: customised environmental chambers, industrial testing applications and organisations requiring manufacturing plus testing expertise. Explore environmental test chambers and their applications in India.
How Do Environmental Chamber Manufacturers Differ?
Not every manufacturer approaches chamber engineering in the same way.
Some manufacturers focus primarily on standard chamber models. These can suit routine laboratory and quality-control applications.
Others provide extensive custom engineering. Custom systems can accommodate unusual product dimensions, higher heat loads, specialised testing profiles or integrated automation.
Testing infrastructure can also create an important difference.
A manufacturer with its own testing facility can better understand real-world qualification requirements. It can also support customers beyond equipment supply.
This is one area where Comet Environs has a distinct positioning. Its manufacturing capabilities are supported by an environmental testing facility. The company provides environmental testing across temperature, humidity, thermal shock, altitude, corrosion, dust and rain-related requirements.
What Should You Check Before Selecting A Manufacturer?
Start with the actual test requirement.
Define the required temperature range. Then establish the humidity range and required stability.
Chamber volume is equally important. The workspace should accommodate the product, fixtures and required airflow.
Next, review controller capabilities. Programmable profiles, data logging, alarms and connectivity can improve testing control and traceability.
Construction quality also matters. Check insulation, interior materials, sensors, airflow and door sealing.
For demanding applications, evaluate custom engineering capabilities. The manufacturer should be able to adapt the chamber to your product and testing requirements.
Finally, assess lifecycle support. Installation, commissioning, calibration, preventive maintenance and spare parts can affect long-term operating performance.
Types Of Chambers Offered By Indian Manufacturers
Indian manufacturers offer different chamber configurations for different testing requirements.
Temperature chambers
Temperature chambers primarily control temperature. They support high-temperature, low-temperature and thermal cycling studies.
Temperature and humidity chambers
Temperature and humidity chambers control both parameters. They are commonly used for climatic testing and product reliability evaluation.
Thermal shock chambers
Thermal shock chambers create rapid temperature transitions. They help identify failures caused by sudden thermal stress.
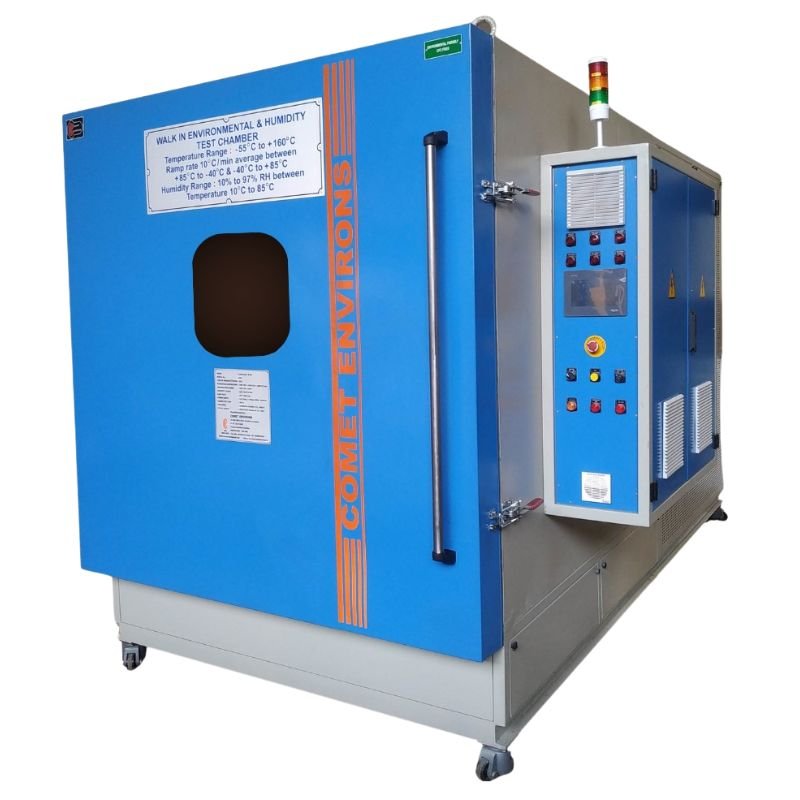
Walk-in chambers
Walk-in chambers accommodate larger products and assemblies. They are useful for automotive, aerospace, defence and industrial applications.
Altitude Test Chambers
Altitude Test Chambers simulate reduced atmospheric pressure conditions. They support testing of products designed for high-altitude environments.
Custom environmental chambers
Custom environmental chambers are designed around specialised testing requirements. These may include EV batteries, aerospace systems, large assemblies or specialised research applications.
Industries Served By Environmental Chamber Manufacturers
In automotive and EV applications, chambers can support testing of batteries, ECUs, sensors and electronic modules.
In aerospace and defence, environmental simulation helps evaluate equipment under temperature, humidity and altitude conditions.
In electronics and semiconductors, testing can assess thermal cycling, moisture exposure and component reliability.
In pharmaceutical and medical applications, controlled environmental conditions support stability and product evaluation.
Industrial manufacturers also use chambers for materials, plastics, packaging and other reliability studies.
Comet Environs currently highlights automotive, EV, aerospace, defence, electronics, semiconductor, pharmaceutical and medical applications.
Environmental Chamber Standards And Testing
Environmental chamber selection should consider the applicable testing standard.
Common standards include the IEC 60068 series, ISO 16750, JEDEC JESD22, ASTM standards and MIL-STD-810.
The correct standard depends on the product and intended test.
The chamber itself should therefore be selected around the required test profile. Temperature range alone should not determine the purchase.
Comet’s environmental testing facility supports MIL, JSS, IS, IEC and ISO testing protocols. Its current NABL scope also covers environmental testing for electronic, electrical, mechanical and electromechanical products.
Why Choose Comet Environs?
Comet Environs brings more than four decades of environmental testing experience.
The company designs and manufactures environmental chambers in India. Its capabilities extend from chamber design and fabrication to installation, commissioning and lifecycle support.
Its biggest advantage is the combination of manufacturing expertise and testing capability.
Comet operates an ISO/IEC 17025:2017 NABL-accredited environmental testing facility. It also states DGAQA certification.
The company also provides customised environmental chamber solutions. Designs can be developed around specific product requirements, environmental conditions, chamber dimensions and testing objectives.
Its portfolio covers standard and specialised systems. These include climate chambers, thermal shock chambers, battery chambers, rapid cycling chambers, walk-in chambers and other environmental simulation systems.
For customers requiring both equipment manufacturing and environmental testing expertise, this integrated approach can provide an important engineering advantage.
Environmental Chamber Manufacturers: Key Takeaway
India has several capable environmental chamber manufacturers. Each manufacturer has different strengths.
Some focus on broad equipment portfolios. Others emphasise testing services or digital controls.
Comet Environs stands out through its combination of manufacturing, custom engineering and testing infrastructure.
With more than four decades of experience, an Indian manufacturing base and an ISO/IEC 17025:2017 NABL-accredited testing facility, Comet is positioned to support both standard and specialised environmental testing requirements.
If you are comparing environmental chamber manufacturers, focus on engineering capability, customisation, testing expertise, standards support and after-sales service.